8 Major CNC Machining Defects Analysis: Causes, Solutions and Prevention
2026-09-16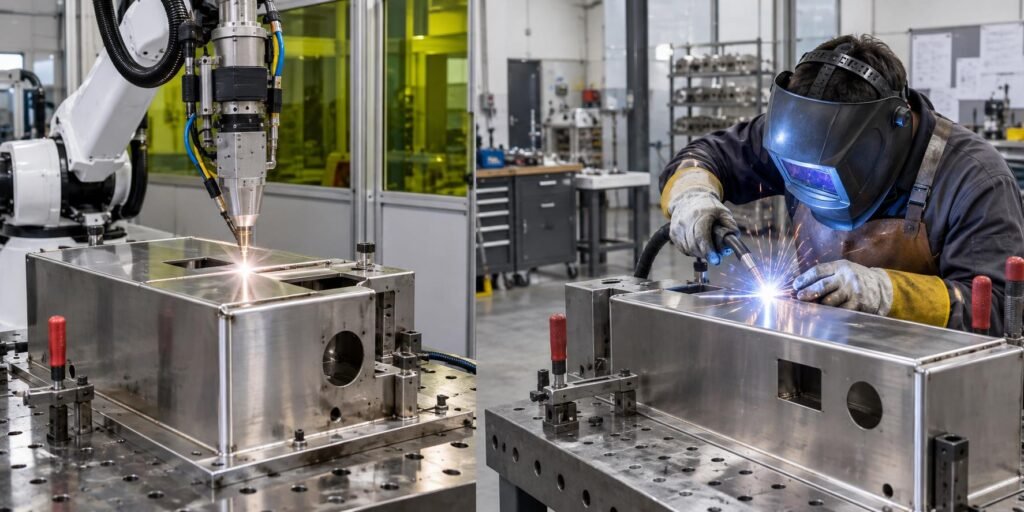
Laser Welding vs MIG Welding: 6 Key Differences and How to Choose
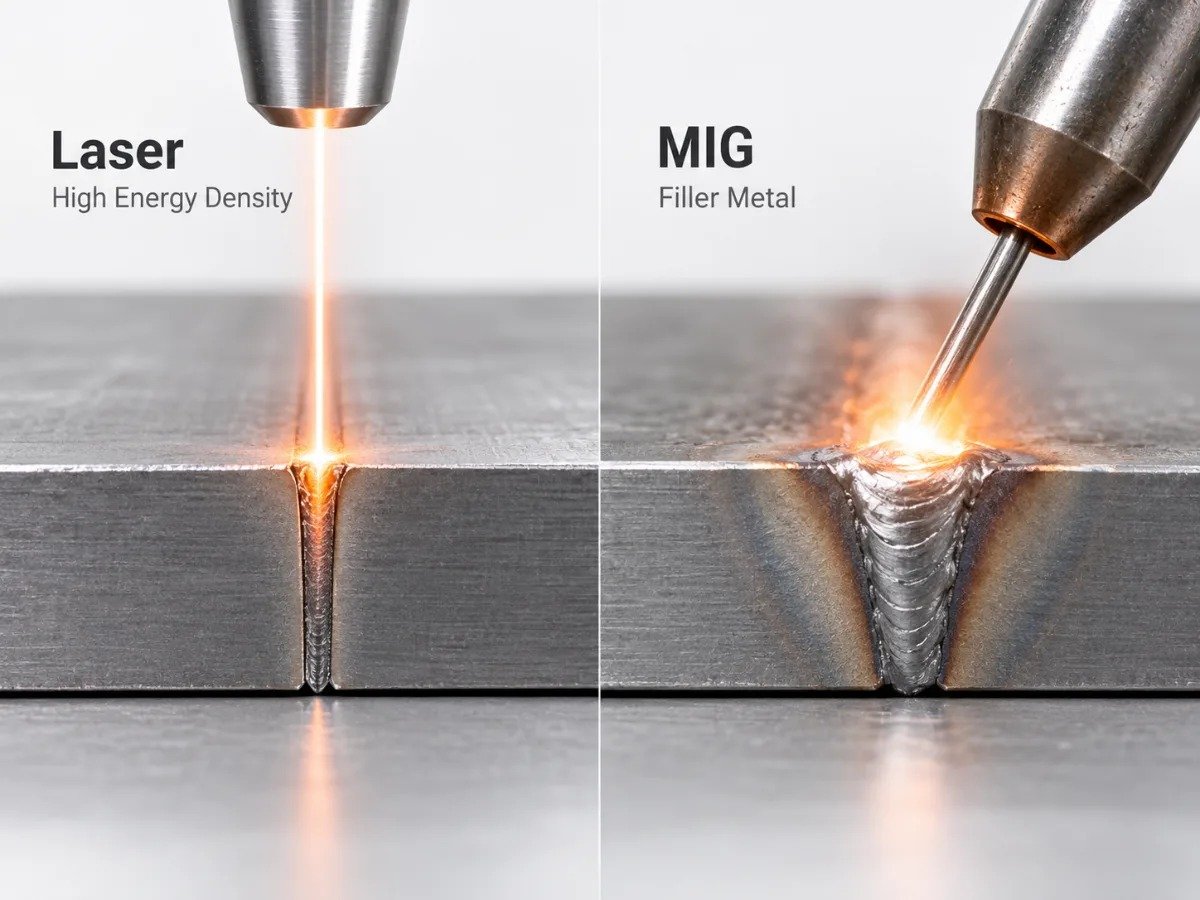
Laser welding vs MIG welding is not simply a contest between a modern process and a conventional one. Laser welding offers concentrated heat, fast travel speed, narrow seams and low distortion. MIG welding offers filler metal, strong gap-bridging ability, broad thickness capability and lower setup cost. The correct choice depends on joint fit-up, material, thickness, production volume, appearance and inspection requirements.
How Laser Welding and MIG Welding Work
What is laser welding?
Laser welding focuses a high-energy beam onto a small area of the joint. The concentrated energy can create a shallow conduction weld or a deeper keyhole weld. In many sheet metal applications, the joint is fused without filler wire, although laser systems can also add wire when gap tolerance or metallurgy requires it.
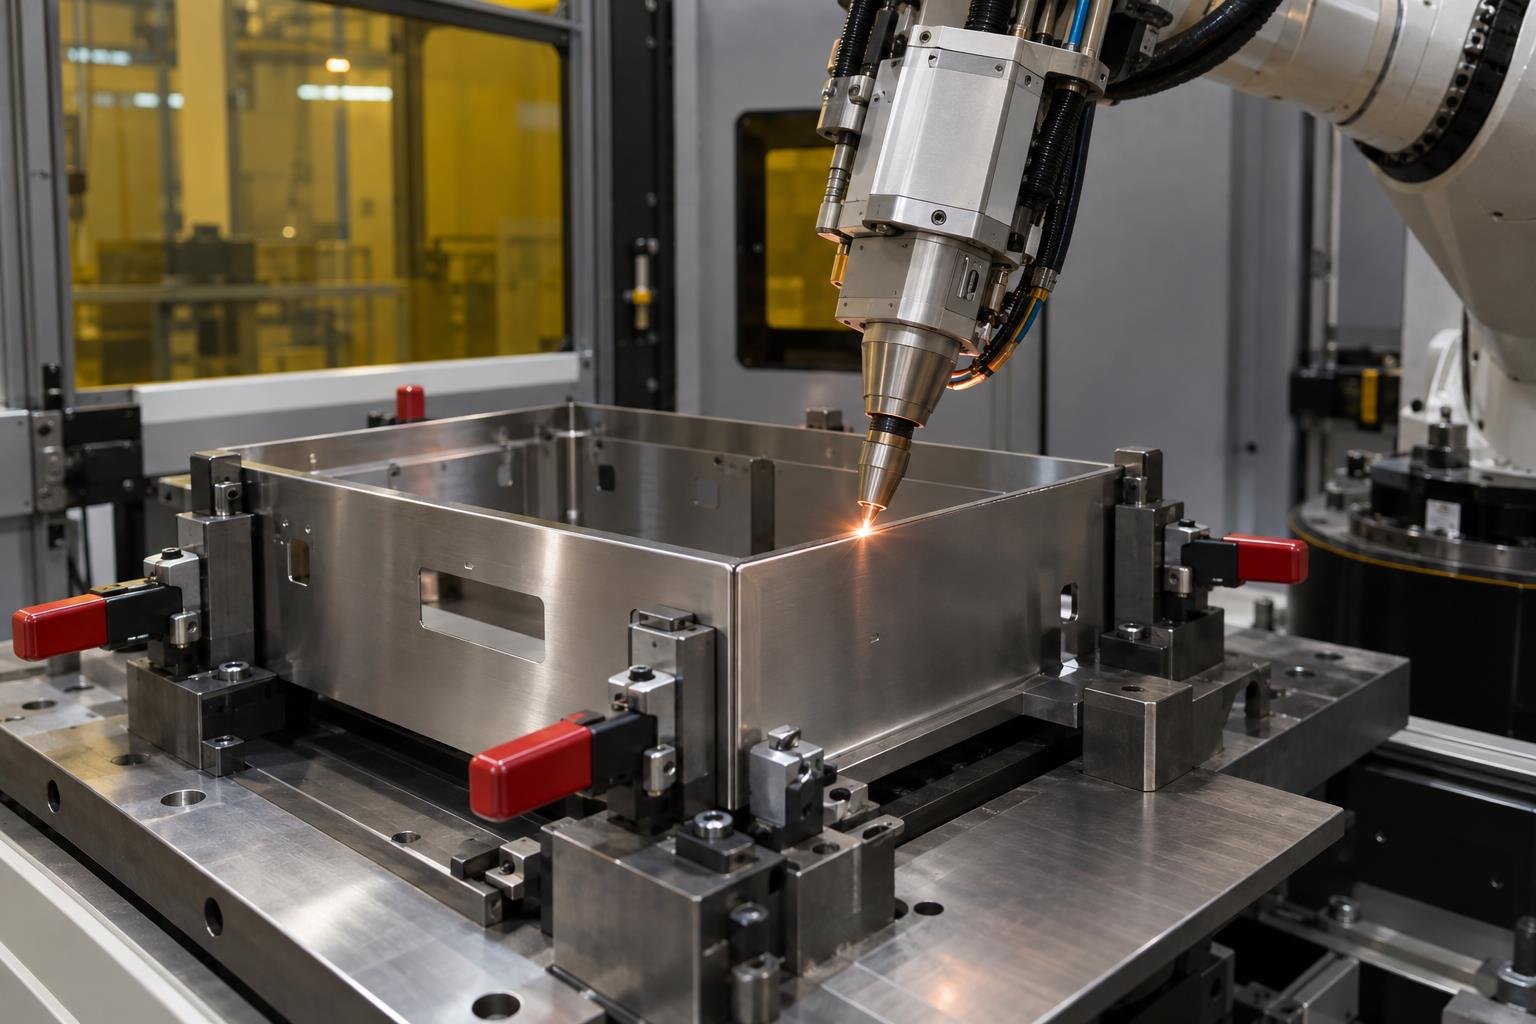
Because the heat source is narrow and controllable, laser welding can achieve high travel speeds with a small heat-affected zone. Robotic motion and seam tracking make it suitable for repeat production, precision enclosures, battery components, medical hardware and stainless steel assemblies.
What is MIG welding?
MIG welding, also called gas metal arc welding or GMAW, creates an electric arc between the workpiece and a continuously fed wire electrode. The wire melts into the joint as filler metal while shielding gas protects the weld pool from atmospheric contamination.
MIG welding is widely used because it is productive, adaptable and easier to deploy than many automated laser systems. It works across fabrication shops, structural assemblies, frames, cabinets, automotive components and repair operations. Process capability depends on wire type, shielding gas, transfer mode, joint preparation and operator or robot control.
Laser Welding vs MIG Welding: Quick Comparison
| Selection factor | Laser welding | MIG welding |
|---|---|---|
| Heat source | Focused laser beam with high energy density | Electric arc with continuously fed wire electrode |
| Joint fit-up | Usually needs tight, consistent gaps and accurate fixturing | Filler wire can bridge larger and less consistent gaps |
| Heat-affected zone | Narrow, with lower overall heat input | Wider heat spread and greater distortion risk |
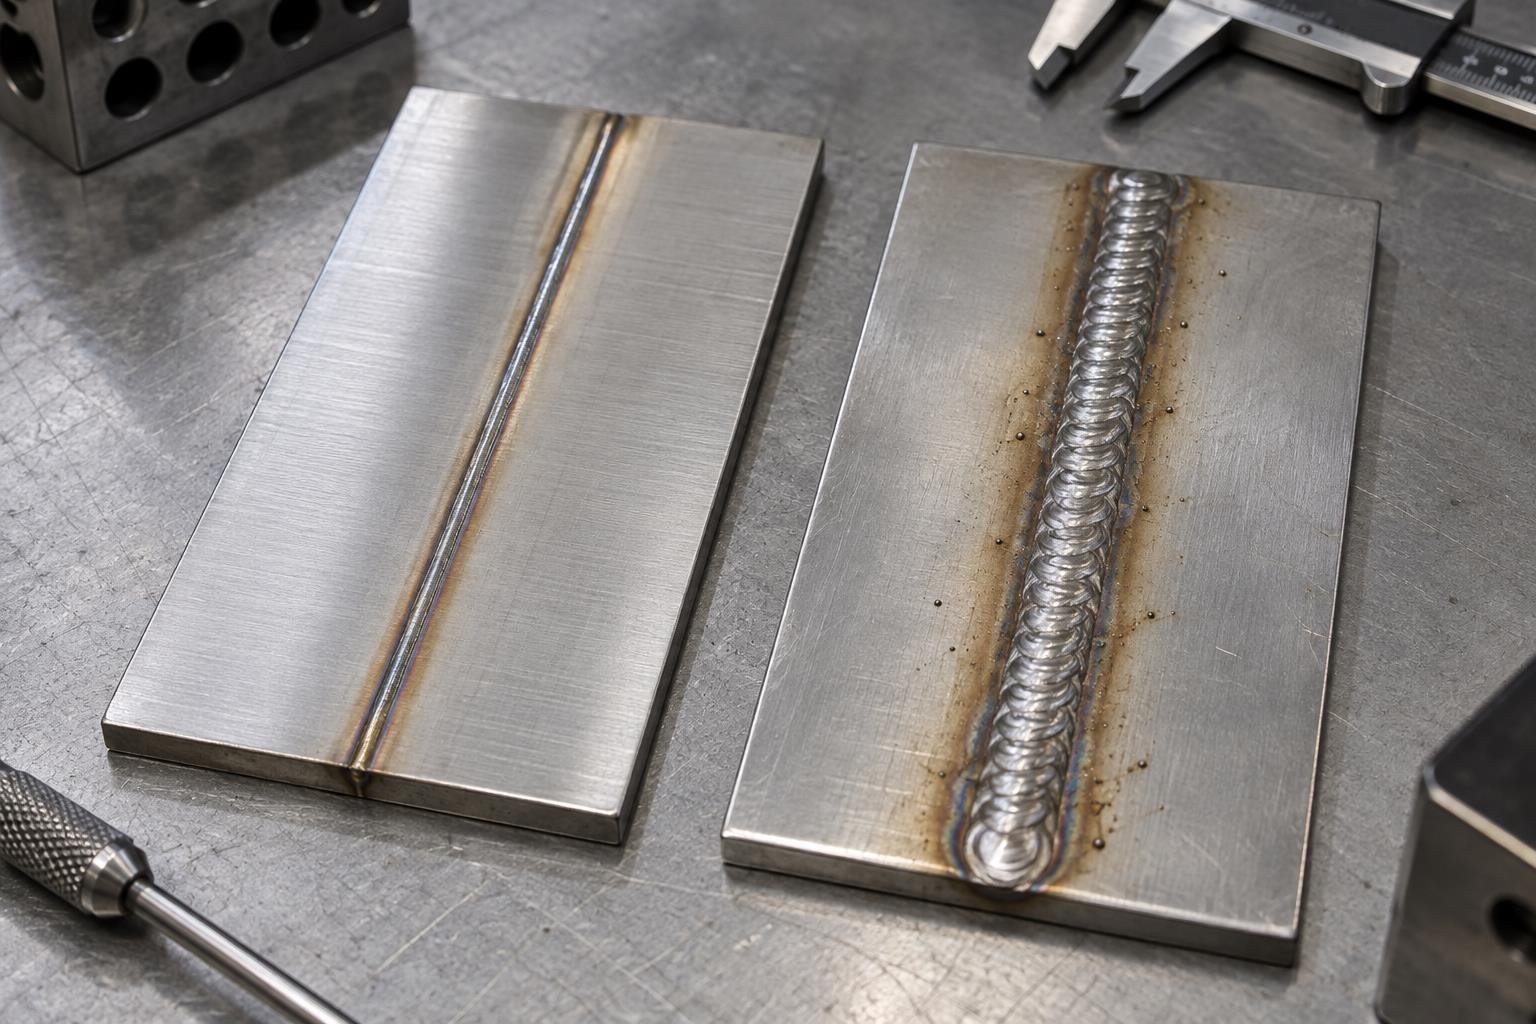
| Weld appearance | Narrow, smooth seam with little spatter | Wider raised bead; spatter and cleanup may be required |
| Thickness range | Excellent for thin and medium precision sections; capacity depends on laser power | Versatile from sheet to heavy sections using bevels and multiple passes |
| Automation | Strong fit for repeatable robotic production | Suitable for manual, cobot and robotic welding |
| Initial investment | High equipment, enclosure, fixture and process-development cost | Lower equipment and setup cost |
| Consumables | Low when welding autogenously; optics and shielding still require control | Wire, shielding gas, contact tips, liners and nozzles |
| Best production pattern | Stable designs, controlled fit-up and medium-to-high repeat volume | High mix, variable fit-up, prototypes, repair and general fabrication |
6 Key Differences Between Laser Welding and MIG Welding
1. Heat concentration and distortion
The laser directs energy into a much smaller area. Less surrounding material is heated, so thin panels and precision assemblies are less likely to bow, twist or pull machined features out of position. MIG welding spreads heat across a wider weld pool. That wider pool is useful for fusion and filler deposition, but it can increase shrinkage and distortion.
This distinction affects the entire process route. When bores, sealing faces or finished surfaces sit close to the joint, laser welding may preserve tolerances that would otherwise require post-weld machining. With MIG welding, engineers often plan the sequence as weld first, then machine critical features after the assembly has stabilized.
2. Joint gap tolerance and fit-up
Fit-up is often the first hard limit. An autogenous laser weld has little material available to fill an opening. If the edges do not meet consistently, the beam may pass through, produce undercut or leave incomplete fusion. Precision cutting, bending and rigid fixtures therefore become part of the laser welding process.
MIG welding continuously adds molten wire. It can accommodate more variation in cut edges, bend angles and assembly gaps. This flexibility is valuable for large fabrications, manual assemblies and low-volume jobs where dedicated precision fixtures would cost more than the parts justify.
3. Welding speed and production rate
On a suitable joint, laser welding can travel quickly and often completes penetration in one pass. Its low spatter and narrow bead can also reduce grinding, straightening and refinishing. The greatest productivity gain is therefore not always arc-on time; it can be the removal of downstream operations.
MIG welding is also productive because wire feeds continuously, but thick sections may require bevel preparation, several passes and interpass cleaning. For short runs, however, MIG can start producing sooner because programming, safety enclosure design, seam tracking and custom fixture development are less demanding.
4. Weld bead, appearance and post-processing
Laser welding typically leaves a narrow, low-profile seam with limited spatter. On stainless enclosures, visible products and hygienic assemblies, this may reduce grinding and polishing. MIG produces a wider, more prominent bead. A well-controlled MIG weld can be visually consistent, but customer-facing surfaces may still need spatter removal, blending or cosmetic finishing.
5. Equipment, labor and operating cost
A laser cell may include the laser source, beam delivery, chiller, fume extraction, safety enclosure, motion system, seam tracking and precision fixtures. Its capital cost is high, but a stable automated process can deliver short cycles and low direct labor per part. Autogenous laser welding also avoids filler wire.
MIG equipment is less expensive and easier to redeploy. Skilled labor, wire, gas, contact tips and cleanup remain recurring costs. The lower entry price usually favors prototypes and changing product mixes, while laser economics improve as repeat volume spreads programming and fixture costs across more parts.
6. Process flexibility and operator dependence
Automated laser welding rewards consistency. Once a joint, fixture and parameter window are qualified, the system can reproduce the same seam at high speed. It is less forgiving when part position, gap, surface condition or beam focus changes.
Manual MIG welding allows a trained welder to respond to gap changes, awkward access and local variation during the weld. That adaptability is a major advantage, but it also means travel speed, torch angle, stick-out and heat input can vary between operators. Robotic MIG reduces this variation while retaining filler-metal capability.
Materials and Thickness: Where Each Process Fits
| Material or condition | Laser welding considerations | MIG welding considerations |
|---|---|---|
| Carbon and mild steel | Fast, clean welding on controlled sheet joints; surface coatings must be considered | Broadly proven for sheet, tube, frames and heavier structures |
| Stainless steel | Excellent for thin precision parts where distortion and appearance matter | Flexible and strong, but heat tint, bead size and distortion may require more control |
| Aluminum | Reflectivity and high thermal conductivity demand suitable laser technology and process development | Requires correct wire, feeding system, cleaning and shielding; commonly used in fabrication |
| Copper | High reflectivity can destabilize absorption; green or blue wavelength systems may improve coupling | High heat conductivity makes heat control difficult; specialized consumables and technique may be needed |
| Coated sheet | Trapped coating vapor can create porosity unless joint design provides an escape path | Coatings can contaminate the weld and generate fumes; preparation and ventilation are essential |
| Dissimilar metals | Rapid, localized heating may help in selected combinations, but brittle intermetallic phases remain a risk | Filler selection may help some combinations, yet many dissimilar joints require a qualified specialist route |
Joint Design and Upstream Manufacturing Requirements
A welding process cannot compensate for a joint that was not designed around its heat source. For laser welding, tolerance accumulation from cutting and bending must keep the seam position and gap inside a narrow window. Tabs, slots, locating features and dedicated clamps can stabilize the joint. For MIG welding, access for the torch, filler deposition and cleaning may require more clearance around the seam.
Design for laser welding
- Keep mating edges accurate and consistent.
- Provide rigid support close to the seam.
- Control part location relative to the beam path.
- Allow shielding gas access and vapor escape.
- Use seam tracking when production variation cannot be eliminated.
Design for MIG welding
- Provide torch angle and nozzle clearance.
- Size bevels and root openings for the required penetration.
- Plan tack sequence to control movement.
- Allow room for multi-pass work and cleanup.
- Specify whether the bead remains visible or will be ground flush.
For broader fabrication planning, review the sheet metal fabrication process and confirm cutting, bending, welding, machining and finishing as one connected route.
How to Compare the Real Cost per Welded Assembly
Machine price alone gives the wrong answer. A meaningful comparison includes all operations required to deliver a conforming part. Laser welding can become economical when high speed and low distortion remove grinding, straightening, rework or post-weld machining. MIG may remain less expensive when production changes often, fit-up varies or a simple fixture and skilled operator can complete the job without extensive engineering.
| Cost element | Questions to include in the quotation |
|---|---|
| Part preparation | Edge cleaning, beveling, cutting tolerance, bend accuracy and pre-weld machining |
| Fixture and programming | Dedicated clamps, robot path, seam tracking, changeover and validation samples |
| Welding cycle | Travel speed, number of passes, tack time, loading and unloading |
| Consumables | Wire, gas, tips, nozzles, optics protection and maintenance items |
| Post-weld work | Grinding, polishing, straightening, heat-tint removal, machining and surface finishing |
| Quality control | Procedure qualification, destructive tests, visual inspection, NDT and dimensional inspection |
| Failure risk | Scrap, repair welding, fixture adjustment and process drift across the production lot |
Weld Quality, Common Defects and Inspection
Both processes can produce strong, repeatable joints when the procedure is matched to the material and design. Defect mechanisms differ, so inspection planning should begin before production.
Typical laser welding risks
- Incomplete fusion when the seam or gap moves outside the beam path
- Undercut from excessive speed or poor parameter balance
- Porosity from contamination, coating vapor or unstable keyhole behavior
- Cracking in sensitive alloys or unsuitable dissimilar-metal combinations
- Insufficient penetration when focus, power or travel speed drifts
Typical MIG welding risks
- Porosity from poor shielding, drafts, moisture or contamination
- Lack of fusion from low heat input or incorrect torch angle
- Excess spatter and undercut from unstable settings
- Distortion from excessive heat or an unbalanced weld sequence
- Wire feeding problems, burnback or inconsistent contact-tip condition
Visual inspection checks bead profile, undercut, overlap, cracks, spatter and surface porosity. Dimensional inspection checks warpage and feature position. Dye penetrant or magnetic particle testing can reveal surface-breaking discontinuities on compatible materials, while radiography and ultrasonic methods can examine internal defects when joint geometry and acceptance requirements justify them. Macro-etch cross sections, peel tests and tensile tests are useful during procedure development.
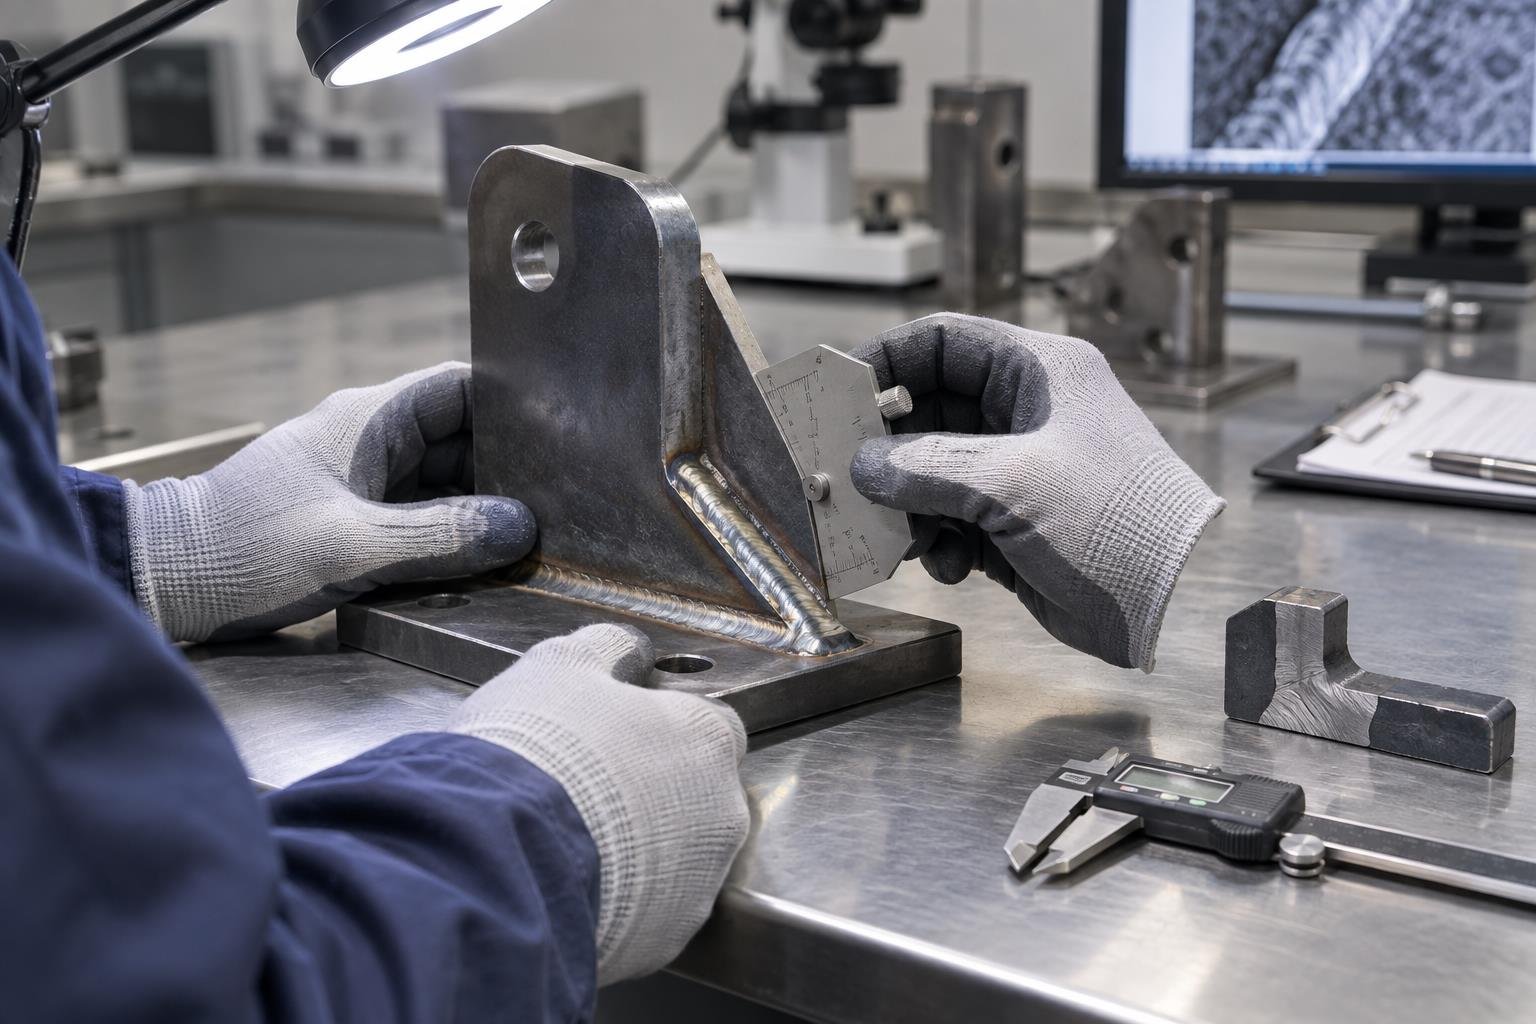
Structural, pressure or regulated work may require a qualified welding procedure specification, procedure qualification record and qualified personnel under the applicable code. Changing from MIG to laser welding can trigger new qualification because heat source, joint behavior and verification methods change.
How to Choose Between Laser Welding and MIG Welding
Measure the real joint gap after cutting, bending and clamping, not only the nominal CAD geometry.
Set penetration, strength, leak tightness, appearance, distortion and inspection requirements.
Include fixture, cycle time, consumables, grinding, straightening, machining and inspection.
Run representative parts, section the joint where necessary and lock the approved parameters.
Choose laser welding when
- The joint has tight, repeatable fit-up.
- Parts are thin or sensitive to distortion.
- A narrow cosmetic seam is valuable.
- Production volume supports automation and fixtures.
- Reducing grinding or post-weld machining offsets capital cost.
Choose MIG welding when
- The assembly has variable gaps or needs filler metal.
- Sections are thick, beveled or require multiple passes.
- Product mix changes often or volumes are low.
- Manual access and repair flexibility are important.
- Lower initial equipment and fixture cost is the priority.
Information to send a welding supplier
- 2D drawing and 3D model with joint location and weld symbols
- Material grade, thickness, temper or heat-treatment condition
- Expected annual quantity and batch size
- Penetration, strength, leak and cosmetic requirements
- Dimensional tolerances near the weld and allowed distortion
- Applicable welding code, inspection method and sampling plan
- Surface finish, coating and whether the weld must be ground flush
FAQ: Laser Welding vs MIG Welding
Is laser welding stronger than MIG welding?
Not automatically. Strength depends on penetration, weld geometry, material, filler selection, defects and loading direction. Either process can meet demanding requirements when the joint and procedure are properly qualified.
Which process causes less distortion?
Laser welding usually causes less distortion because heat is concentrated into a narrow zone and travel speed can be high. Part geometry, restraint and weld sequence still matter, so a laser-welded assembly is not guaranteed to remain perfectly flat.
Can laser welding fill a gap?
Autogenous laser welding has limited gap-bridging capability. Laser systems can add filler wire or use beam oscillation, but these options do not remove the need for controlled fit-up. MIG welding generally tolerates wider and more variable gaps.
Which process is better for aluminum?
Both can weld aluminum. Laser welding requires equipment and parameters that manage reflectivity and rapid heat conduction. MIG welding requires clean material, appropriate wire, stable feeding and correct shielding. The best choice depends on alloy, thickness, joint fit-up, appearance and volume.
Is laser welding cheaper for mass production?
It can be. High travel speed, automation and reduced cleanup may lower total unit cost after fixtures and process development are amortized. A cost study should compare the complete manufacturing route, not only welding time.
Can one drawing support both processes?
Sometimes, but process-specific access and fit-up requirements can differ. Drawings should prioritize measurable performance requirements such as penetration, bead limits, distortion and inspection level. Specify the process when a code, customer requirement or qualified procedure makes it mandatory.
Need a Welded Metal Assembly Reviewed?
Milemetal supports precision metal parts, sheet metal fabrication, welding, machining and finishing. Send the drawing, material, quantity and quality requirements for a manufacturing review.
Reference: This original Milemetal guide was developed after reviewing the process-selection framework in RapidDirect’s laser welding vs MIG welding comparison. The structure, wording, examples, tables and recommendations were independently expanded for OEM metal-part buyers and engineers.