CNC Turning Services for Precision Shafts, Bushings, Fittings and Round Parts
Milemetal provides custom CNC turning services for prototypes, low-volume production and repeat manufacturing. We machine precision turned parts from aluminum, stainless steel, carbon steel, alloy steel, brass, bronze, copper, titanium and engineering plastics, including shafts, pins, sleeves, spacers, nozzles, threaded fittings and complex lathe components.
Custom CNC Turning Capabilities
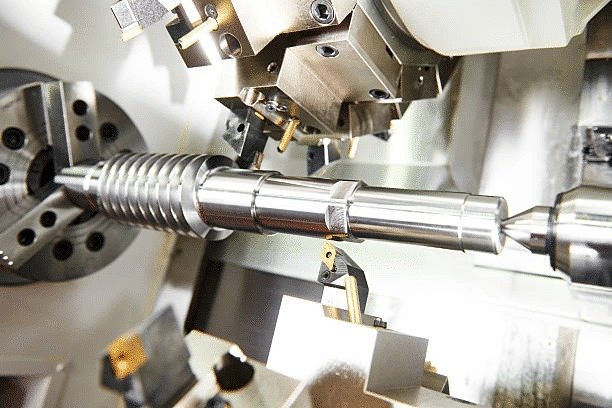
CNC turning uses a rotating workpiece and controlled cutting tools to create round or rotationally symmetric geometry. It is highly efficient for producing accurate outside diameters, inside bores, grooves, tapers, faces, chamfers, knurls and threads. Modern turning centers can also drill, mill flats, machine cross holes and create wrench flats using live tooling.
Turning is often the best process when the part is based on a shaft, sleeve, ring, spacer, nozzle, connector or bushing. For parts that combine round geometry with pockets or side holes, CNC turning can be combined with CNC milling in the same setup or through secondary operations.
Accurate outside diameters, steps, tapers, shoulders and bearing surfaces.
Internal bores, counterbores, bushings, sleeves and precision hole finishing.
Internal and external metric, UNC, UNF, BSP, NPT and custom thread features.
O-ring grooves, retaining-ring grooves, relief grooves and cutoff operations.
Cross holes, flats, slots and light milling features on turned components.
Small diameter, long, slender and high-repeatability parts with close feature control.
Related Manufacturing Processes
CNC turning is often reviewed together with other manufacturing routes during early DFM. For milled flats, pockets and multi-side features, compare our CNC milling services. For broader precision machining support, see CNC machining services. For long, slender and small-diameter parts, review Swiss-type CNC machining design guidance. For plating, passivation, anodizing, polishing and marking, compare surface finishing services. You can also review typical CNC turning parts before sending an RFQ.

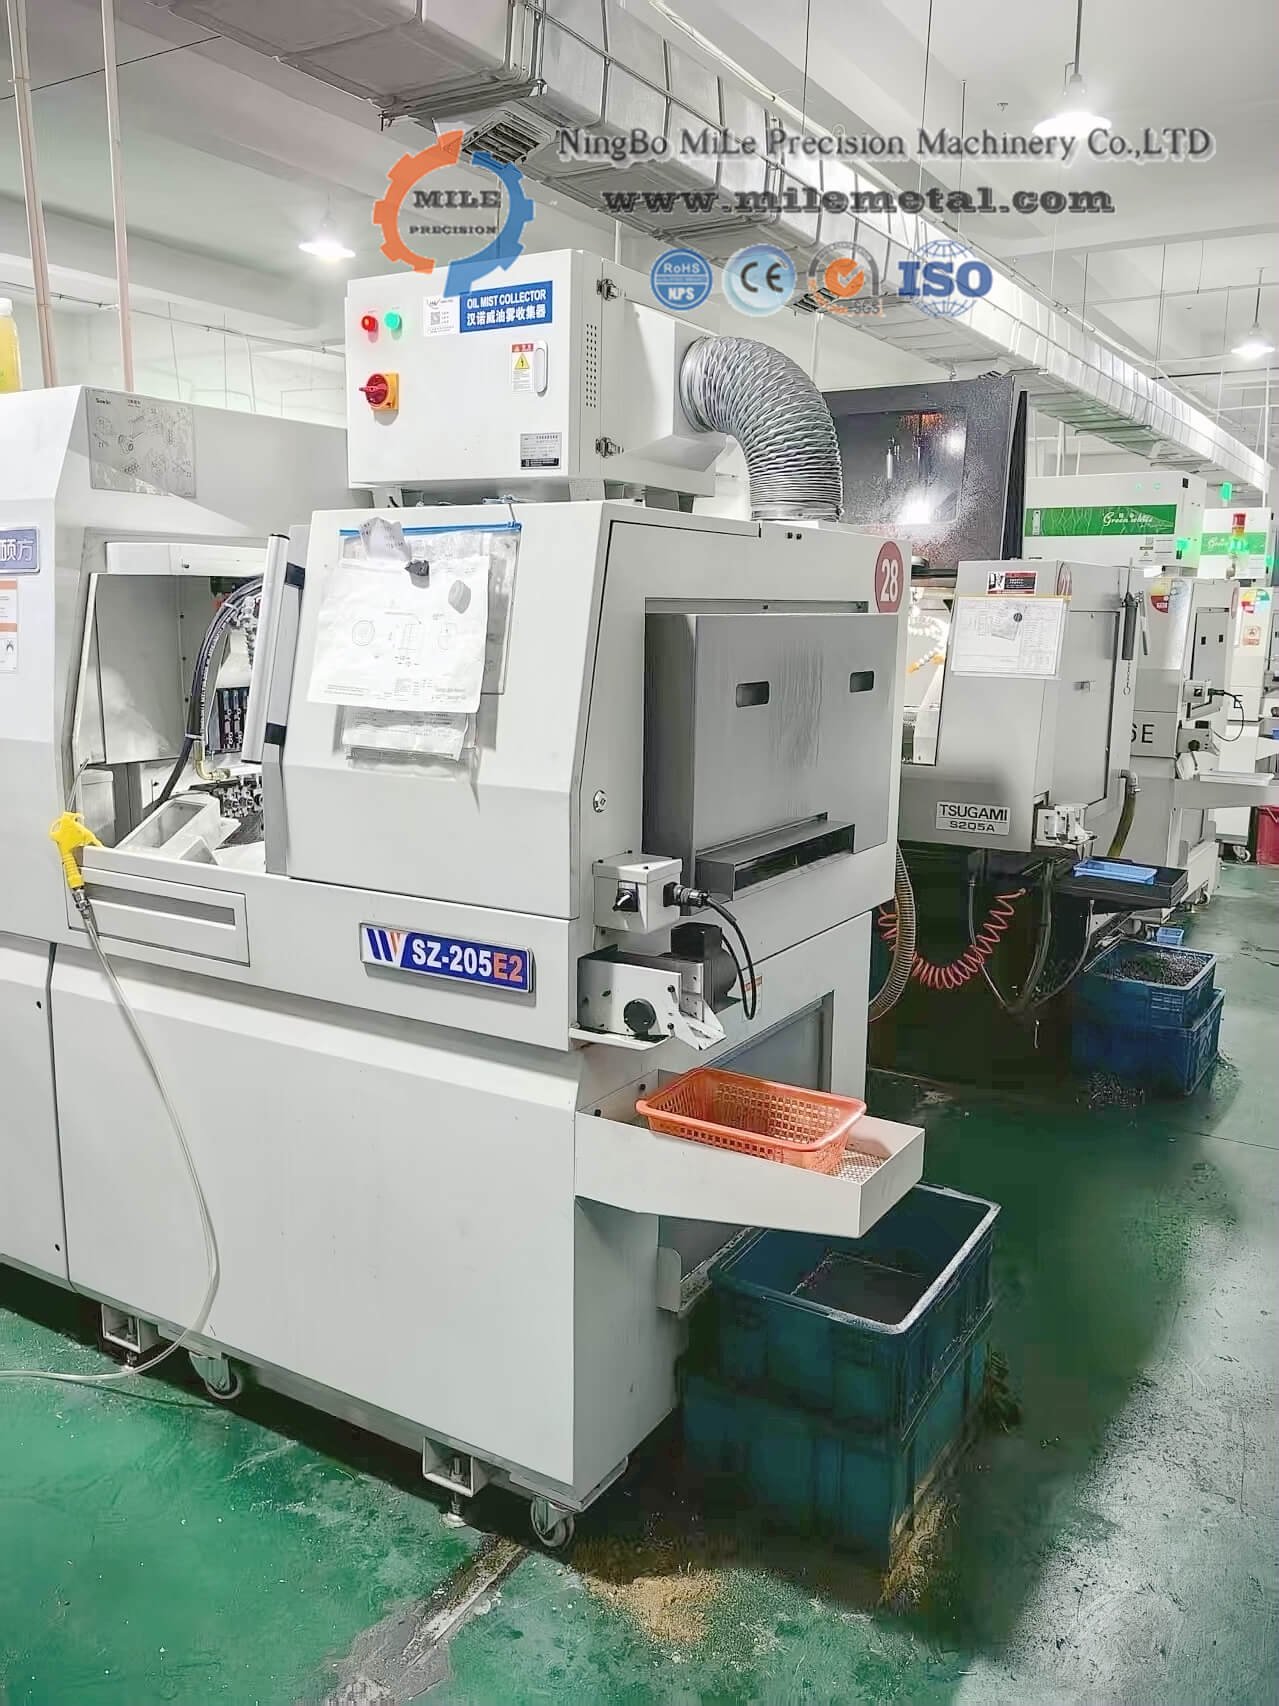
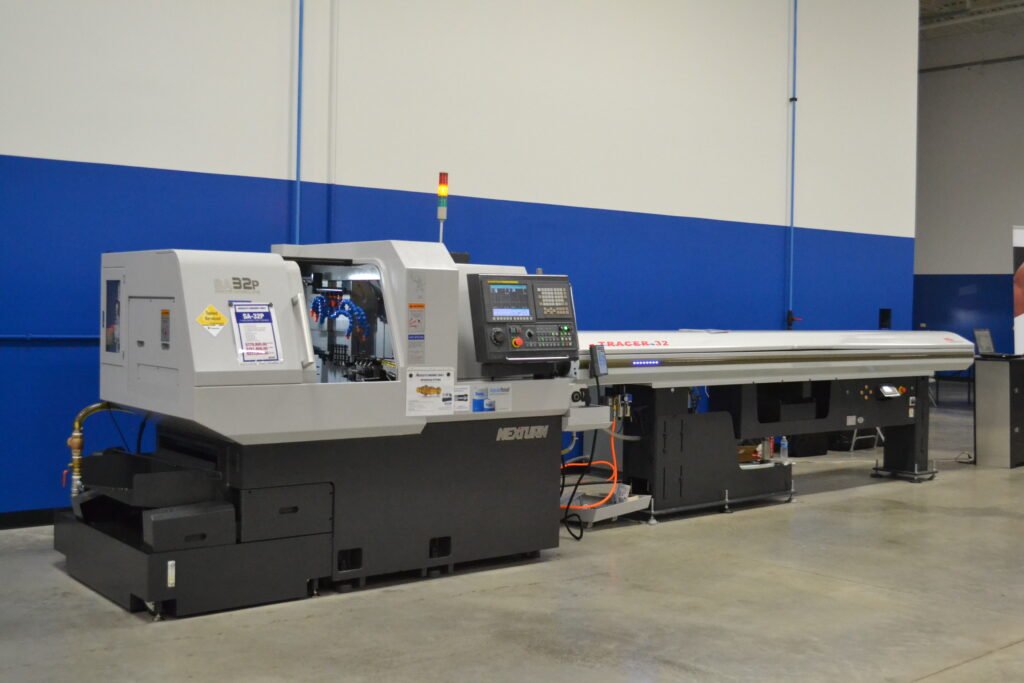
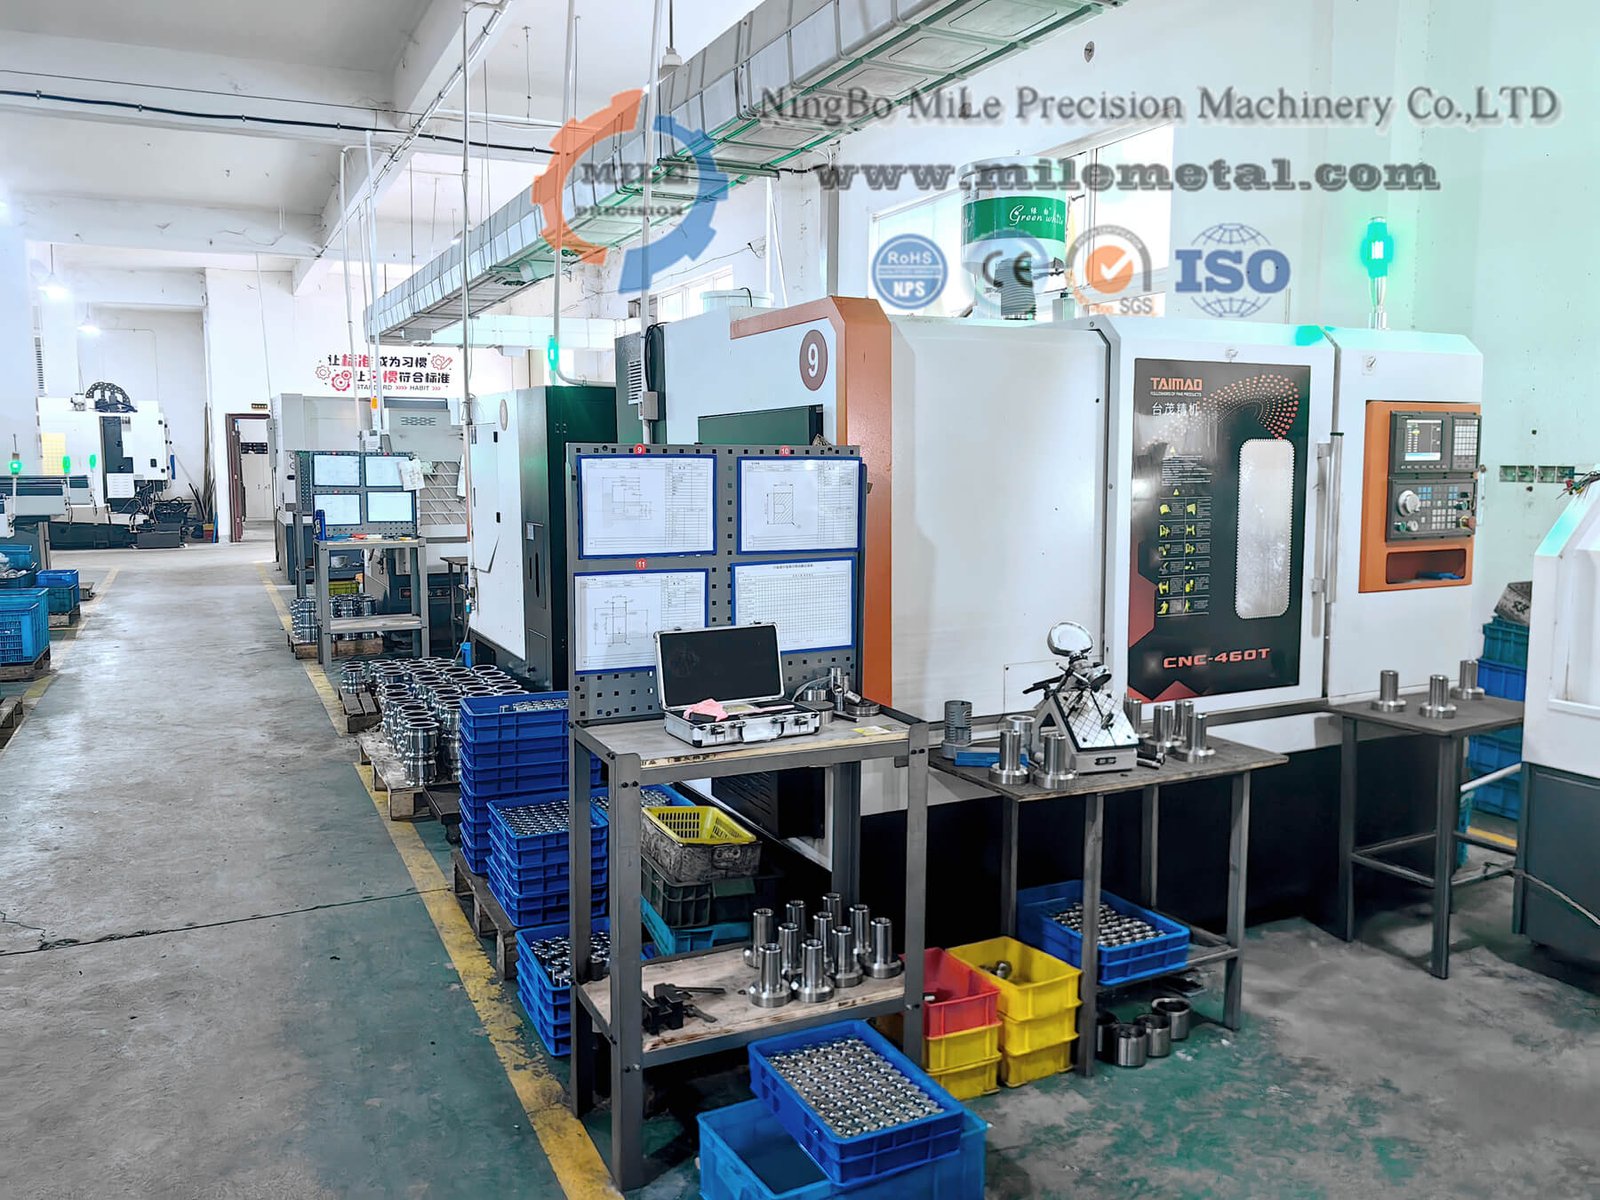
CNC Turning in Action
Real machining footage and finished parts
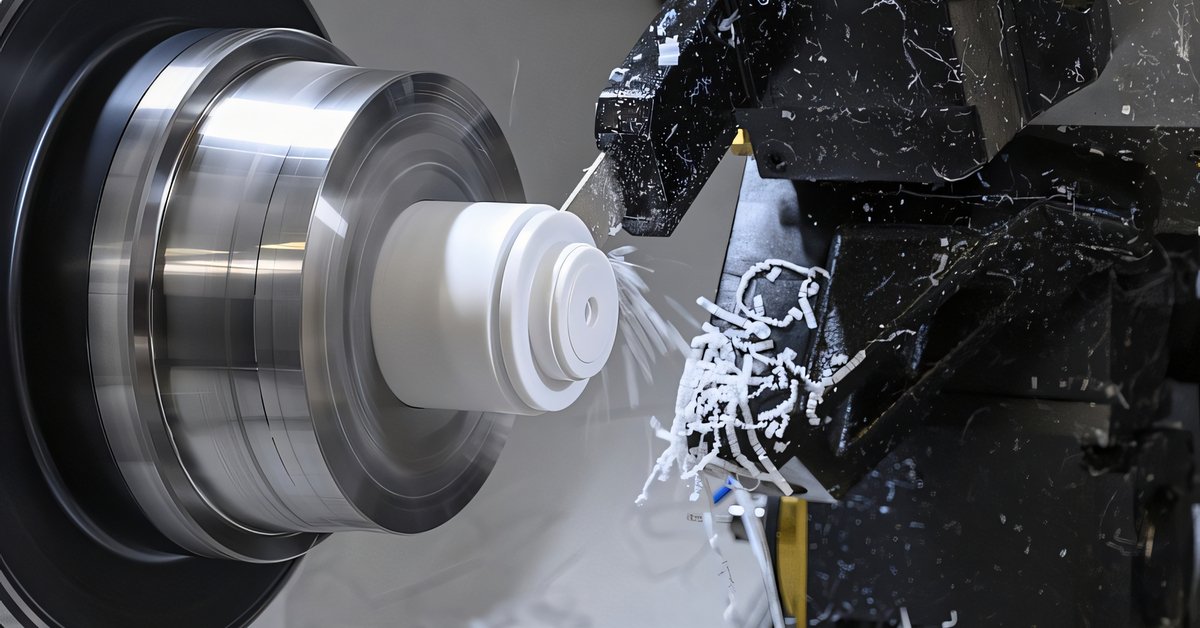
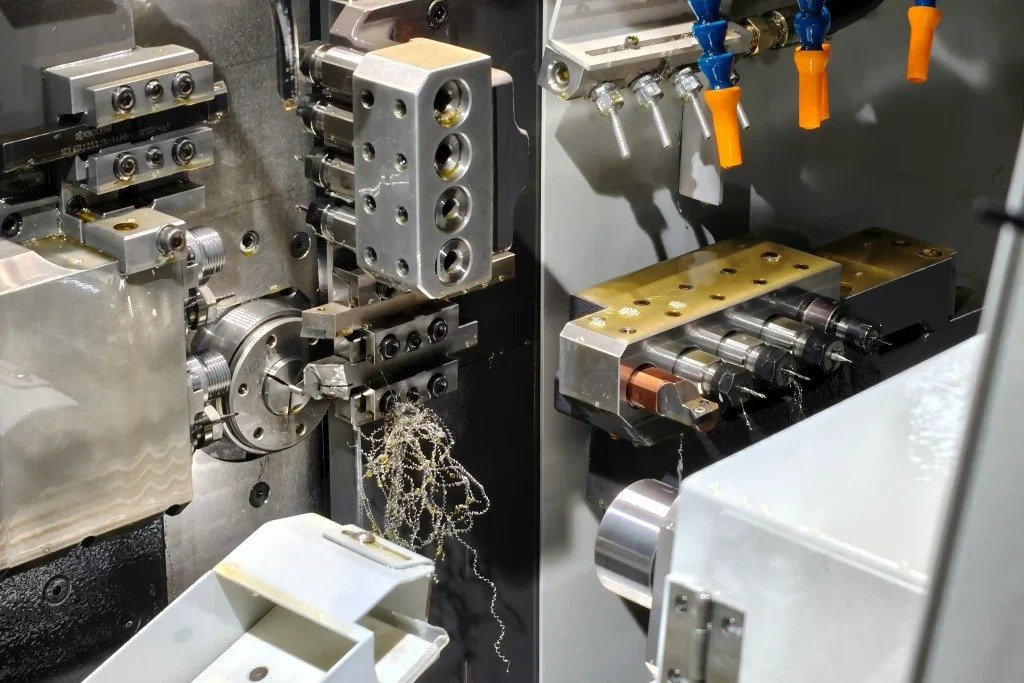
Watch Milemetal’s CNC turning process and product showcase. This video brings the machining operation and the resulting components together, alongside the turning capabilities and part examples on this page.
Planning a similar component? Send your CAD model and drawing with the material, quantity, critical dimensions and surface finish requirements for a machining review.
CNC Turned Parts Gallery
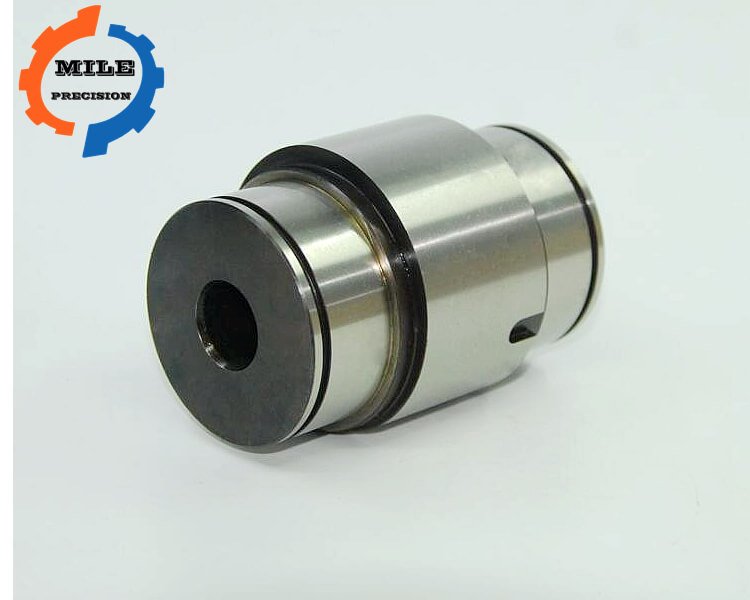
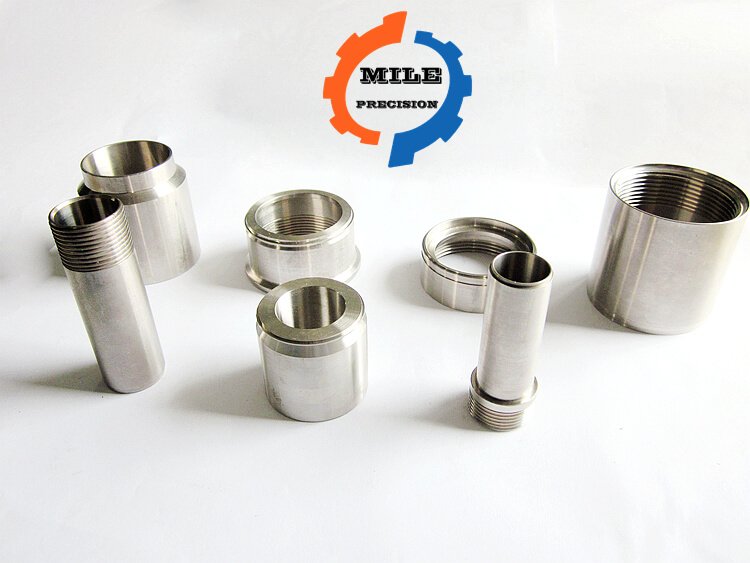
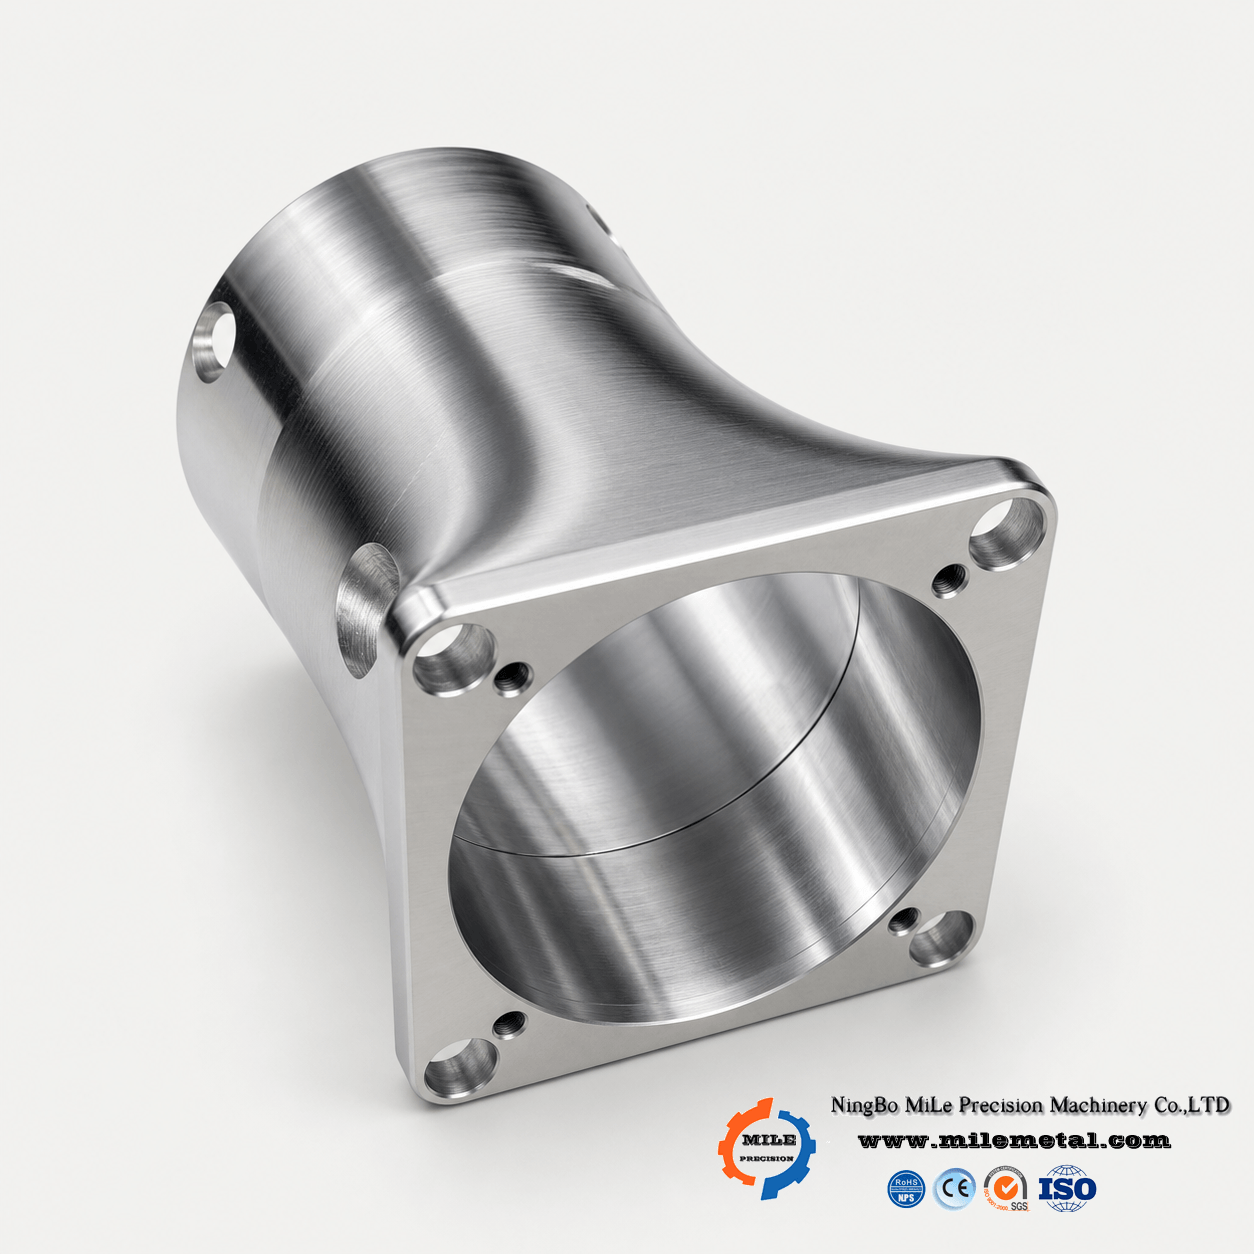
Typical CNC turned parts include shafts, pins, sleeves, rings, bushings, fittings, nozzles, spacers, rollers and custom cylindrical components. The examples below show common turned-part requirements such as thread quality, bore accuracy, surface finish, concentricity and burr-free edges.





CNC Turning Process Flow
Drawing review
Review diameter tolerances, thread standards, runout, material, surface finish and heat treatment notes.
Setup and tooling
Select chucking, collet, bar feed, support, inserts, drills, boring tools and thread tools.
Turning operations
Machine faces, diameters, bores, grooves, tapers, chamfers, threads and part-off features.
Inspection and finish
Check diameters, threads, concentricity, runout, surface finish and final packaging.
CNC Turning Technical Capability Table
| Capability | Typical features | Practical guideline | Design note |
|---|---|---|---|
| Outside diameter turning | Steps, tapers, bearing journals, shoulders | +/-0.01 to +/-0.03 mm possible on selected diameters | Define functional diameter and inspection location clearly |
| Internal boring | Bores, sleeves, counterbores and inside steps | Deep small bores increase tool deflection and chatter | Allow practical bore depth and provide relief where possible |
| Thread turning | External and internal threads | Metric, UNC, UNF, BSP, NPT and custom forms possible | Specify thread length, class, gauge requirement and coating allowance |
| Grooving | O-ring grooves, snap-ring grooves and relief cuts | Groove width and corner radius depend on insert selection | Use standard groove dimensions when possible |
| Knurling | Grip patterns and press-fit texture | Pattern depth depends on material and tool pressure | Define cosmetic or functional requirement before production |
| Live tooling | Cross holes, flats, slots and simple milled features | Reduces secondary setup for turned parts | Best for moderate side features on round parts |
| Swiss turning | Small pins, inserts, connectors and slender shafts | Excellent for long small-diameter parts | Material straightness and bar quality are important |
CNC Turning Materials
Material choice affects chip control, tool wear, burr formation, surface finish, dimensional stability and cost. Turned parts often have threads, bores or sealing surfaces, so material and finishing should be selected together.
| Material | Common grades | Turning behavior | Typical turned parts |
|---|---|---|---|
| Aluminum | 6061, 6082, 7075, 5052 | Fast turning, good finish and suitable for anodizing | Spacers, housings, sleeves, knobs and lightweight shafts |
| Stainless steel | 303, 304, 316, 316L, 17-4 PH | Needs sharp tools, coolant and work-hardening control | Nozzles, fittings, medical parts, sealing components and fluid hardware |
| Carbon / alloy steel | 1018, 1045, 4140, 42CrMo4 | Strong and heat treatable; hardness affects cutting speed | Shafts, rollers, pins, axles, threaded studs and mechanical parts |
| Brass / bronze | C360, C260, bearing bronze | Excellent machinability and good chip control | Inserts, bushings, fittings, spacers, gears and connectors |
| Copper | C101, C110, tellurium copper | Ductile and conductive; may smear without correct tooling | Electrical contacts, electrodes, heat transfer parts and conductive pins |
| Engineering plastics | POM, nylon, PTFE, PEEK, ABS, PC | Low cutting force but sensitive to heat and clamping pressure | Insulators, rollers, bushings, spacers and low-friction parts |
CNC Turning Tolerances and Design Parameters
Turning can hold excellent roundness and diameter control when the part is properly supported. Long slender parts, deep bores, thin walls and interrupted cuts need special review because they can vibrate, deflect or move after machining.
| Feature | Typical guideline | Risk factor | Recommendation |
|---|---|---|---|
| General turned diameter | +/-0.05 to +/-0.10 mm is practical for many non-critical features | Low | Use tighter tolerances only on functional fits |
| Precision journal or bore | +/-0.01 to +/-0.03 mm possible for selected features | Medium to high | Specify fit, surface finish and inspection method |
| Concentricity / runout | Depends strongly on setup and datum strategy | High | Machine related diameters in one setup when possible |
| Long slender shafts | Length-to-diameter ratio above 8:1 needs review | High | Use center support, steady rest or design changes |
| Deep internal bores | Depth above 4x bore diameter can increase chatter | High | Increase bore diameter, shorten depth or allow larger tolerance |
| Surface finish | Ra 3.2, Ra 1.6 and Ra 0.8 are common turning targets | Medium | Apply fine finish only to sealing, bearing or visible surfaces |
Relative CNC Turning Difficulty Chart
The chart below compares common materials from a practical turning point of view. Geometry, tolerance, length, bore depth and thread requirements may change the final cost.
Design Tips for CNC Turned Parts
Keep datums logical
Define which diameter or face controls runout, concentricity and assembly fit.
Avoid extreme slenderness
Long thin shafts can bend during cutting and shipping; support strategy matters.
Use standard threads
Standard thread sizes, reliefs and chamfers reduce tooling cost and inspection risk.
Plan grooves carefully
O-ring and retaining-ring grooves need correct width, depth, radius and surface finish.
- Send STEP files and PDF drawings with diameter tolerances, thread callouts and surface finish notes.
- For press fits or bearing journals, define fit class and inspection method.
- For plated or anodized turned parts, account for coating thickness on threads and bores.
- For sealing parts, define Ra value, flatness and acceptable burr condition.
- For long parts, discuss straightness and support before production.
Surface Finishing Options for CNC Turned Parts
| Finish | Common material | Purpose | Turning design consideration |
|---|---|---|---|
| As machined | Most metals and plastics | Fast functional finish with visible turning marks | Define edge break and burr limits for grooves and threads |
| Anodizing | Aluminum | Color and corrosion protection | Mask precision bores or threads if coating thickness affects fit |
| Passivation | Stainless steel | Improve corrosion resistance after machining | Useful for fluid, medical and food equipment parts |
| Electroless nickel plating | Steel, aluminum, copper alloys | Uniform corrosion and wear protection | Account for plating thickness on journals and threaded features |
| Heat treatment | Steel, alloy steel, 17-4 PH | Increase hardness, strength or wear resistance | Plan rough turning, heat treatment and finish grinding if needed |
| Polishing | Stainless, aluminum, brass, copper | Improve appearance and reduce roughness | Specify sealing or visible surfaces only to control cost |
Quality Control for CNC Turning
Turned parts often fail because of runout, thread problems, burrs inside holes or incorrect surface finish. Inspection should focus on the features that control assembly, sealing, rotation and wear.
| Inspection item | Common method | When to use |
|---|---|---|
| Diameters and bores | Micrometer, bore gauge, pin gauge, CMM | Bearing seats, sleeves, press fits and precision shafts |
| Thread quality | Thread plug gauge, ring gauge and visual inspection | Internal threads, external threads and pipe fittings |
| Runout and concentricity | Dial indicator, V-blocks, CMM | Rotating parts, shafts, journals and mating diameters |
| Surface finish | Roughness tester and visual inspection | Sealing faces, sliding diameters and cosmetic surfaces |
| Burr and cleanliness | Visual inspection, borescope, cleaning check | Fluid parts, medical parts, small holes and threaded features |
Applications of CNC Turning
CNC turning is widely used for parts that rotate, seal, slide, guide, locate or connect. It is suitable for prototypes, low-volume production and repeat batch manufacturing.
| Application area | Typical turned parts | Important requirement |
|---|---|---|
| Industrial machinery | Shafts, rollers, pins, spacers and bushings | Diameter tolerance, straightness, wear resistance and runout |
| Fluid and pneumatic systems | Nozzles, fittings, ports, valve stems and threaded adapters | Burr-free holes, sealing surfaces, pressure integrity and thread quality |
| Electronics and instruments | Connectors, sleeves, knobs, conductive pins and small housings | Surface finish, conductivity, plating and small feature repeatability |
| Medical and laboratory equipment | Stainless shafts, precision fittings and plastic spacers | Clean surfaces, corrosion resistance and dimensional traceability |
| Automotive and hardware | Fasteners, inserts, bushings, collars and custom adapters | Batch consistency, thread inspection, heat treatment and finishing |
How to Choose a CNC Turning Supplier
A reliable CNC turning supplier should review the drawing, not only the outside diameter and length. The team should confirm datum strategy, concentricity, thread standards, groove details, material behavior, finishing effects and inspection methods before production. This is important for overseas buyers who need stable quality, clear communication and repeatable turned parts across batches.
| Evaluation point | What to check | Why it matters |
|---|---|---|
| Turning capability | Can the supplier handle shafts, bushings, sleeves, fittings, nozzles, threaded parts and Swiss-type small components? | Different part families need different workholding, tool access and inspection planning. |
| Tolerance planning | Does the team review concentricity, runout, diameter tolerance, groove width, thread fit and surface finish? | Round parts often fail because relationships between features are not controlled clearly. |
| Material experience | Has the supplier turned stainless steel, aluminum, brass, copper, alloy steel, titanium and engineering plastics? | Material behavior affects tool wear, burrs, deformation, finish and dimensional stability. |
| Secondary machining | Can cross holes, flats, slots, milling features, drilling, tapping and deburring be handled after turning? | Many turned parts require milling or drilling features before they are ready for assembly. |
| Quality control | Are micrometers, calipers, pin gauges, thread gauges, CMM and roughness checks available? | Inspection confirms diameters, threads, position, surface finish and batch consistency. |
| RFQ communication | Does the supplier confirm revision, quantity, lead time, heat treatment, finishing, packaging and unclear notes? | Clear communication reduces rework and delivery risk for international orders. |
Ordering CNC Turned Parts: Fits, Threads and Acceptance
For shafts, sleeves and fittings, a correct diameter alone does not establish assembly performance. A CNC turning enquiry should identify the mating component, reference axis and final surface condition. Use the following checklist to make quotations and inspection results easier to compare.
| Turned part feature | Specify on the drawing | Confirm during quotation |
|---|---|---|
| Bearing journals and mating bores | Diameter limits or fit designation, reference datums and surface roughness. | The measurement method and whether the requirement applies after plating or heat treatment. Include the mating-part specification if available. |
| Long shafts and thin sleeves | Overall length, supported surfaces, wall thickness and straightness or runout requirements. | Workholding and support strategy, inspection condition and whether the part must be measured free of clamping loads. |
| Threaded fittings and ports | Thread standard, nominal size, pitch, tolerance class, usable depth and sealing method. | The appropriate thread gauge and acceptance criteria. A thread designation alone does not define the complete sealing interface. |
| Grooves, cross holes and milled flats | Groove location, edge condition and angular relationships to other features. | Secondary milling, burr removal at intersecting holes and protection of sealing or sliding surfaces. |
Plan acceptance around the mating assembly
If a turned part rotates, seals, slides or locates another component, identify that function in the RFQ. Diameter, roundness and runout are different controls; specify the requirement that protects the assembly. Agree the datum setup and any functional gauge before production, and state whether first-piece results or a final dimensional report are required.
Published precision values describe selected features under suitable conditions. Confirm the complete diameter-and-length envelope, material condition and post-finish requirements for your part. The quote should distinguish sample approval, machining, outside finishing and shipping time.
CNC Turning Purchasing FAQs
Should my component use CNC turning or CNC milling?
Turning is a natural starting point for parts organised around a common axis, such as shafts, sleeves and bushings. Flats, side holes or slots may require live tooling or a secondary milling operation. For mainly prismatic parts, review our CNC milling service and send the full geometry for process selection.
When should I ask about Swiss-type turning?
Ask for a process review when small, slender parts require support close to the cutting area or repeat production is sensitive to deflection. Diameter, length, material, feature access and quantity determine suitability; a small part does not automatically require a Swiss-type machine.
Can I order matching shafts and bushings together?
Send both drawings, identify the mating diameters and state the intended clearance or interference. Explain the operating conditions and whether components must be interchangeable across a batch or supplied as matched sets.
What should I provide for plated threaded parts?
Include the thread specification, plating type and thickness, masking requirements and final acceptance method. State whether the thread must pass its specified gauge after plating so that machining allowances and inspection can be reviewed together.
How to Get an Accurate CNC Turning Quote
For a reliable quote, send a STEP model and a PDF drawing. The drawing should define diameter tolerances, threads, material, finish, heat treatment, quantity and inspection requirements. For long or thin parts, include straightness and runout expectations.
3D CAD
STEP, Parasolid or native CAD file for geometry and tooling review.
Drawing
PDF drawing with diameter tolerance, thread callouts, runout and surface finish.
Material and quantity
Grade, bar size, prototype or batch quantity and delivery target.
Finish and inspection
Plating, passivation, anodizing, heat treatment, CMM report or gauge inspection needs.
Start Your CNC Turning Project
Send your CAD model, drawing, material, quantity and finish requirements. Milemetal can review manufacturability and provide a practical CNC turning quotation.