Laser Welding vs MIG Welding: 6 Key Differences and How to Choose
2026-09-22
Precision Turned Components for the Connector Industry: Materials, Tolerances & Plating
2026-10-15
Custom Aluminum Enclosure CNC Machining: Design, Materials, Tolerances and Finishing Guide
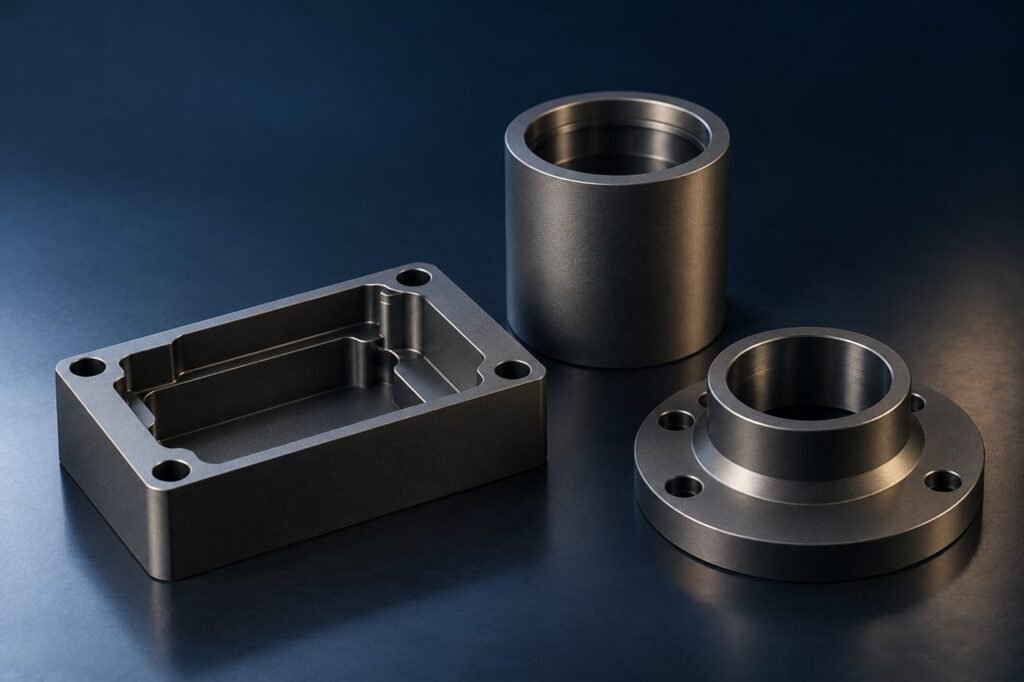
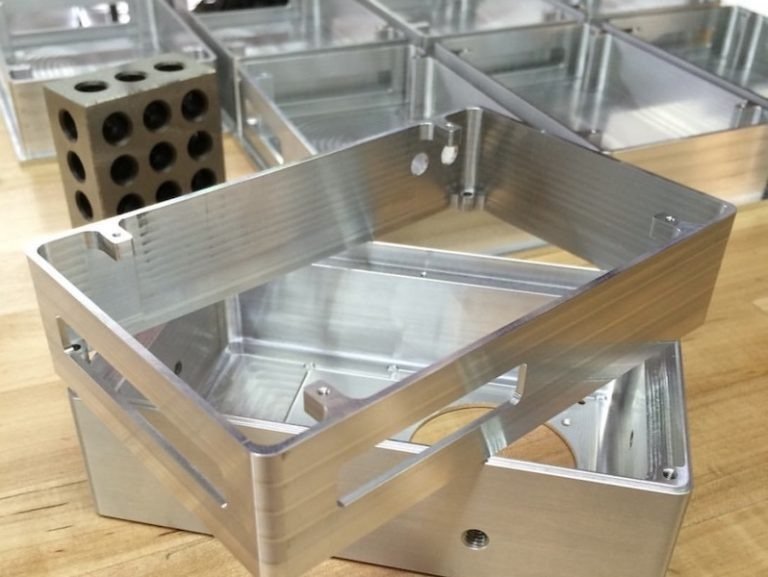
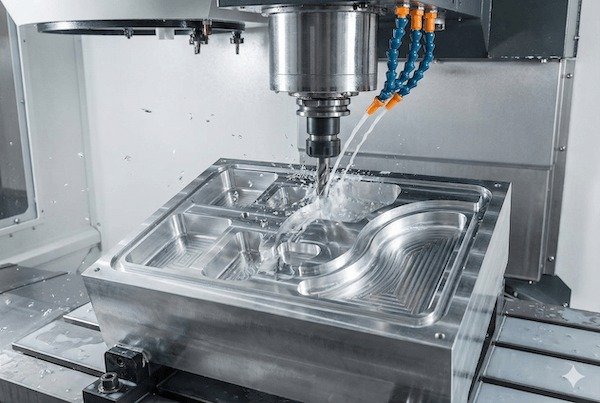
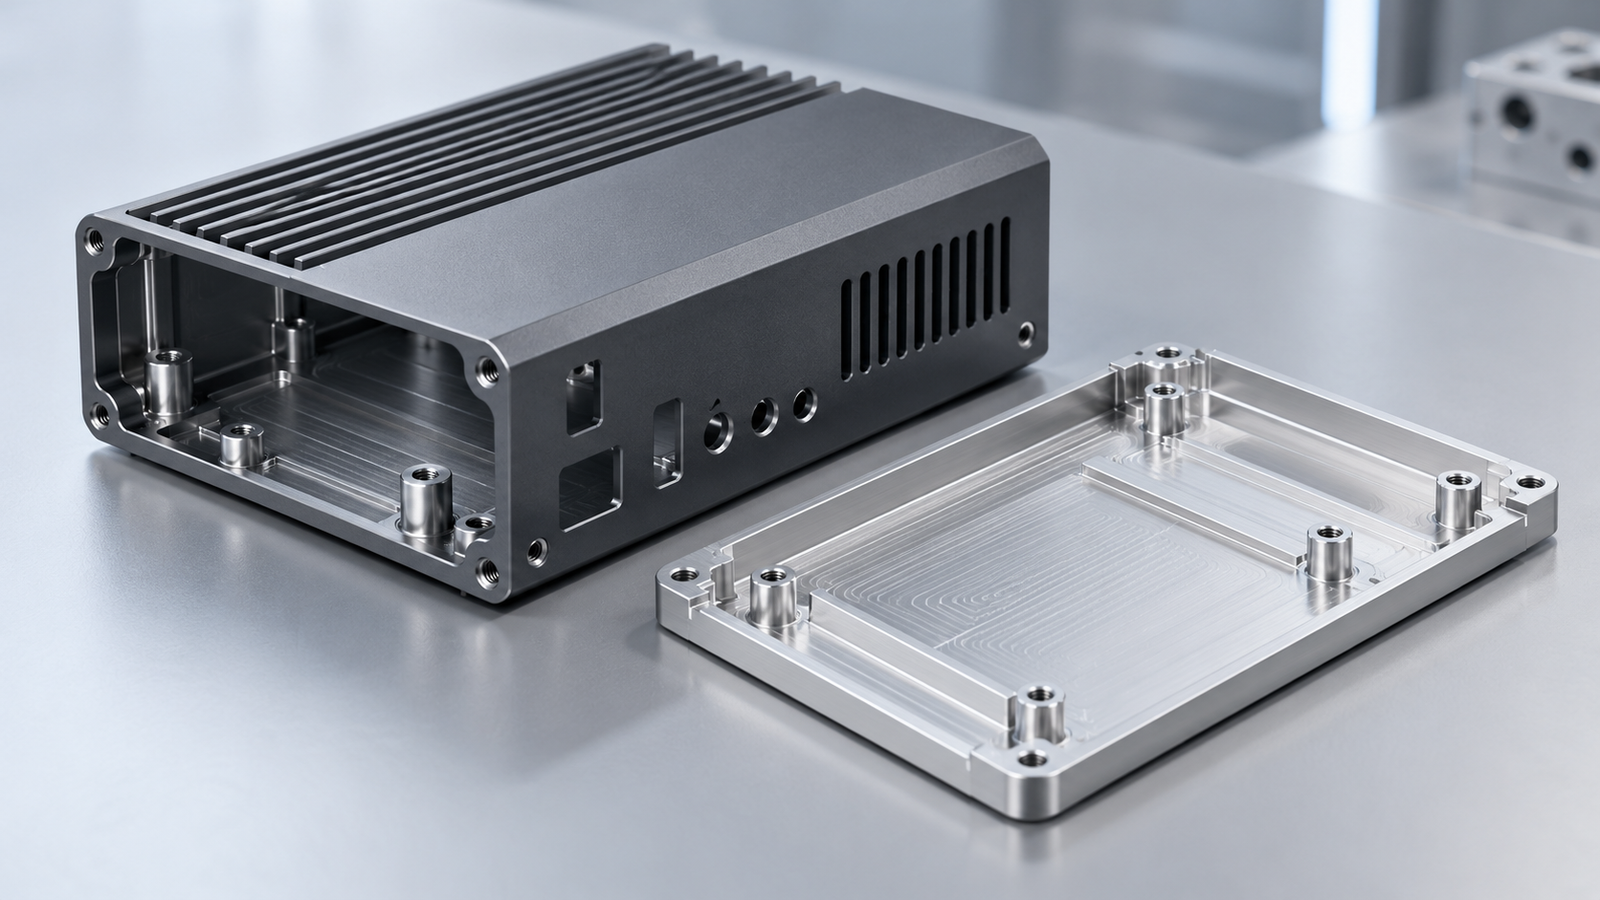
Custom aluminum enclosure CNC machining is a practical choice for electronics housings, controller cases, communication modules, instruments, heat-sink enclosures and industrial equipment covers. Compared with die casting or standard extrusions, CNC machined aluminum enclosures require no mold investment, support fast design changes, and allow complex internal pockets, thin walls, precision holes and high-quality cosmetic surfaces.
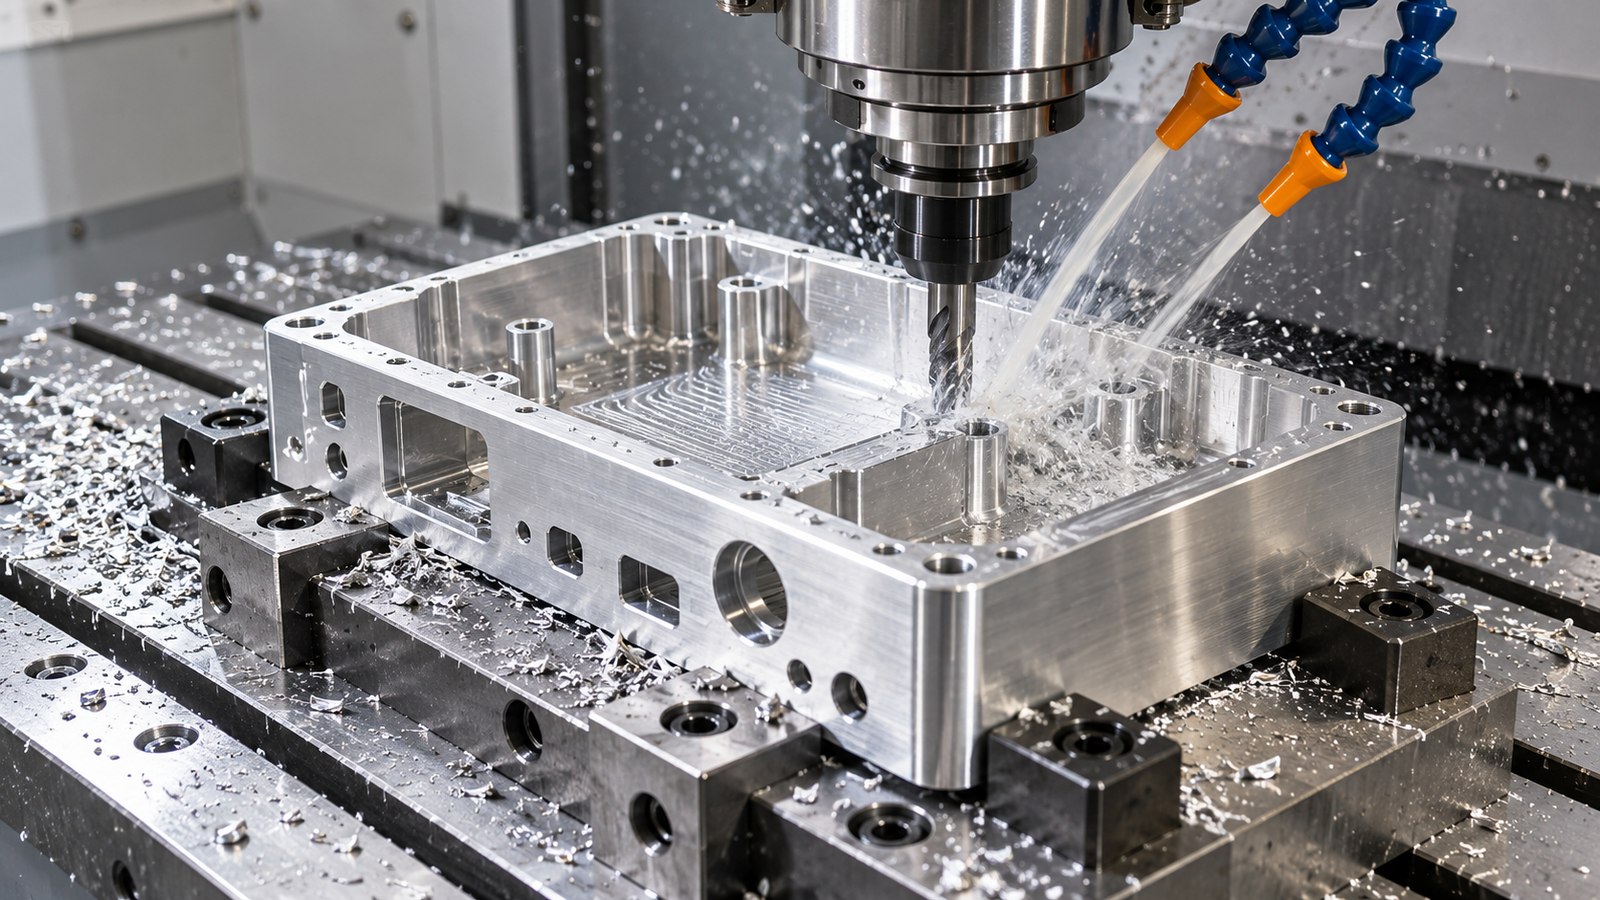
Why Choose CNC Machining for Custom Aluminum Enclosures?
Aluminum offers a strong strength-to-weight ratio, good thermal conductivity, excellent machinability and many finishing options. For projects that need fast structural validation, connector changes, accurate assembly features or a premium metal appearance, CNC machining is often more flexible than mold-based manufacturing.
Suitable for one-off prototypes, pilot runs and small batches without paying for die-casting or extrusion tooling.
Supports pockets, bosses, heat-sink ribs, blind holes, threads, gasket grooves and multi-side connector cutouts.
Machined enclosures can be bead blasted, anodized, chromate converted, brushed, painted or laser marked.
If the product design is stable and annual volume is very high, die casting or extrusion may reduce unit cost. During development, pilot production, multi-model programs or B2B industrial equipment builds, CNC aluminum enclosures usually help teams move from CAD to assembly testing faster.
Common Aluminum Grades for CNC Enclosures: 6061, 6063, 5052 and 7075
Material selection affects strength, machining stability, surface finish, thermal performance, cost and lead time. The best aluminum grade is not always the strongest one; it should match the operating environment, assembly method and cosmetic requirements.
| Aluminum grade | Typical enclosure applications | Advantages | Design notes |
|---|---|---|---|
| 6061-T6 | Electronics housings, instrument cases, fixtures, general structural enclosures | Balanced strength, good machinability, stable anodizing results, wide availability | Deep thin-wall pockets still need careful fixturing and distortion control |
| 6063 | Cosmetic housings, heat-sink profiles, panels and decorative enclosure parts | Good extrusion behavior and attractive anodized surface quality | Lower strength than 6061; load-bearing designs should be reviewed |
| 5052 | Corrosion-resistant covers, sheet aluminum housings, humid or marine-adjacent environments | Good corrosion resistance and formability for sheet structures | Less suitable than 6061 for thick-block enclosures with complex milled pockets |
| 7075-T6 | High-strength brackets, lightweight frames, loaded housings and performance equipment | High strength-to-weight ratio for demanding structural parts | Higher cost; corrosion resistance and anodized appearance should be confirmed early |
| 6082 | Machine enclosures, structural frames, automation parts and European-spec projects | Balanced strength and machinability | Stock size and local availability should be checked before quoting |
CNC Machining Parameters and Tolerance Guidelines for Aluminum Enclosures
The main challenge in enclosure machining is rarely one isolated dimension. More often, quality depends on thin-wall distortion, multi-side location, hole position, assembly clearance, finishing thickness and cosmetic surface protection. The values below are practical starting points for RFQ and design review; final requirements should follow the drawing, material, size and inspection method.
| Requirement | Common guideline | Where it applies | Design reminder |
|---|---|---|---|
| General linear tolerance | +/-0.05 mm to +/-0.10 mm | Outer dimensions, steps, standard holes and non-critical features | Avoid applying +/-0.01 mm to every non-critical dimension |
| Precision assembly features | +/-0.01 mm to +/-0.03 mm | Bearing seats, dowel holes, gasket surfaces and critical hole spacing | Define datums and inspection methods clearly |
| Minimum wall thickness | Typically 1.0 mm to 1.5 mm and above | Small electronics housings, covers and side walls | Large deep-pocket enclosures may need thicker walls or ribs |
| Internal corner radius | At least the cutter radius; common values include R0.5-R3.0 | Internal pockets, step roots and heat-sink grooves | Sharp internal corners increase cost and may require EDM or special processes |
| Threaded holes | M2-M8 are common for enclosure assembly | PCB mounting, cover screws and equipment installation | Specify effective thread depth, especially for blind holes |
| Surface roughness | Ra 1.6-3.2 is common; finer finishes are possible | Cosmetic surfaces, sealing surfaces and assembly faces | Bead blasting changes the visual texture and may not suit sealing faces |
| Anodizing thickness | Standard anodizing is often about 5-20 microns; hard anodizing can be thicker | Appearance, corrosion resistance, wear resistance and insulation | Consider coating thickness on holes, slots, threads and mating surfaces |
Surface Finishing Options: Anodizing, Chromate Conversion, Bead Blasting and Brushing
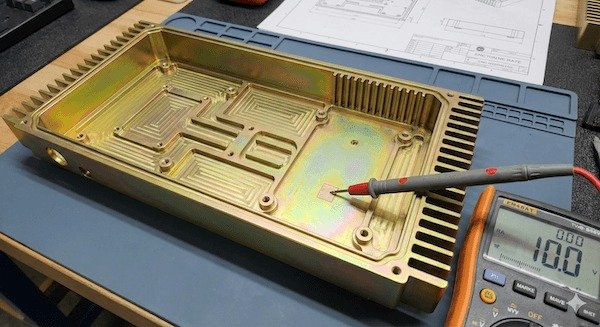
Surface finishing affects more than color. It can change corrosion resistance, electrical conductivity, wear behavior and final dimensions. When ordering custom aluminum enclosures, specify the cosmetic grade, color sample, masking areas, conductive contact areas and packaging requirements.
Common finishing choices
- Clear or color anodizing: Suitable for electronics, instrument housings and controller cases that need stable appearance and corrosion resistance.
- Hard anodizing: Useful for higher wear resistance, corrosion resistance or electrical insulation.
- Chromate conversion: Suitable for EMI shielding, grounding contact, communication equipment and conductive surfaces.
- Bead blasting plus anodizing: Helps create a more uniform cosmetic texture, but changes surface roughness.
- Brushing, polishing and painting: Useful for brand-facing surfaces or special color and texture requirements.
DFM Checklist: 8 Ways to Reduce CNC Aluminum Enclosure Cost
Many aluminum enclosure cost drivers come from tight tolerances, deep pockets, very small tools, repeated setups and finishing rework rather than material alone. Early DFM review can reduce machining time and quality risk without weakening the product function.
Design pocket corners around available cutter radii instead of sharp internal corners.
Deep thin walls can chatter or distort; add ribs or thickness where possible.
Only tighten tolerances on sealing, locating and assembly-critical features.
Fewer thread sizes reduce tool changes, inspection complexity and batch variation.
Align holes, covers, PCB mounts and gasket grooves around clear datum references.
Anodizing affects holes, slots, threads and mating faces.
Deep small holes and deep threads increase tool breakage risk and cycle time.
Define A, B and non-cosmetic surfaces for handling, finishing and inspection.
CNC Aluminum Enclosures vs Die Casting, Extrusions and Sheet Metal
No manufacturing process is best for every project. The right choice depends on volume, geometry, cosmetic requirements and product stage. The comparison below helps engineering and sourcing teams select the right path.
| Manufacturing method | Best volume range | Advantages | Limitations | Typical uses |
|---|---|---|---|---|
| CNC machined aluminum enclosure | Prototype to small and medium batches | No tooling, fast revision, high accuracy, flexible structure | Longer cycle time per part; not always lowest cost at very high volume | Prototypes, pilot runs, industrial electronics, instruments, custom equipment |
| Die-cast aluminum enclosure | High volume | Low unit cost after tooling, suitable for complex outer shapes | High mold cost, longer revision cycle, precision features may still need CNC machining | Consumer electronics, lighting housings, mass-production communication equipment |
| Extruded aluminum enclosure | Medium to high volume with fixed cross-section | Good heat dissipation, flexible length, consistent appearance | Cross-section is limited by extrusion tooling; ends and interfaces still need machining | Power supply housings, rail devices, heat-sink boxes, modular enclosures |
| Sheet aluminum enclosure | Prototype to production | Cost-effective for large thin-wall boxes | Less suitable for sealed thick-wall bodies and complex internal pockets | Control boxes, cabinets, equipment covers and panel assemblies |
What to Provide When Requesting a CNC Aluminum Enclosure Quote
Complete RFQ data improves quotation accuracy and reduces engineering back-and-forth. For custom aluminum enclosures, provide both a 3D model and a 2D drawing when possible: the 3D file supports CAM programming and geometry review, while the drawing defines tolerances, material, finishing and critical inspection requirements.
STEP, STP, IGES, X_T and PDF drawings with revision number and units.
Aluminum grade, temper, prototype quantity, pilot quantity and annual demand.
Anodizing color, bead-blast texture, conductive areas, masking notes and laser marking content.
Assembly holes, gasket grooves, PCB mounts, threads, cosmetic faces and inspection datums.
Target delivery date, split shipment needs, individual wrapping and scratch protection.
Indoor or outdoor use, temperature, corrosion exposure, heat transfer, EMI, insulation or grounding needs.
Why Work with Milemetal for Custom CNC Aluminum Enclosures?
Milemetal supports overseas buyers with CNC machining, CNC milling, surface finishing, related assembly parts and small-batch production. For aluminum enclosure projects, our team can review DFM, material choice, fixturing, machining sequence, finishing risks and inspection requirements before production.
If your project also includes shafts, copper components, sheet metal parts, die-cast parts or other precision mechanical components, review our CNC machining parts and surface finishing capabilities, or send drawings directly for engineering review.
Frequently Asked Questions
What production volumes are suitable for CNC aluminum enclosures?
CNC machining is suitable for one-off prototypes, small-batch pilot production and medium-volume manufacturing. If the design is stable and volume is very high, die casting, extrusion or CNC secondary machining may be worth comparing.
Can a CNC aluminum enclosure be designed for sealing or water resistance?
Yes. The design should include an O-ring groove, controlled sealing surface, appropriate screw spacing and sufficient cover stiffness. Surface roughness, flatness and anodizing thickness should be defined early.
Does anodizing change final dimensions?
Yes. Anodizing adds coating thickness and can affect holes, grooves, threads and mating surfaces. Critical areas can be controlled by dimensional allowance, post-machining or masking.
Can you quote from only a 3D model?
Yes, a preliminary quote is possible from a 3D model. For production, a 2D drawing is recommended to define material, tolerances, finishing, threads, critical dimensions, cosmetic surfaces and inspection requirements.
Need a Custom CNC Aluminum Enclosure?
Send your STEP model, PDF drawing, quantity, material and finishing requirements. Milemetal can help review the machining plan, cost risks and lead time.